ManufacturerChoosing the best cuticle scissors manufacturer in China requires more than comparing catalog photos and factory prices. A reliable supplier should demonstrate consistent workmanship, clear communication, and practical knowledge of professional manicure tools. This guide explores manufacturers that produce sharp, balanced, and durable cuticle scissors for salons, distributors, and private-label brands.
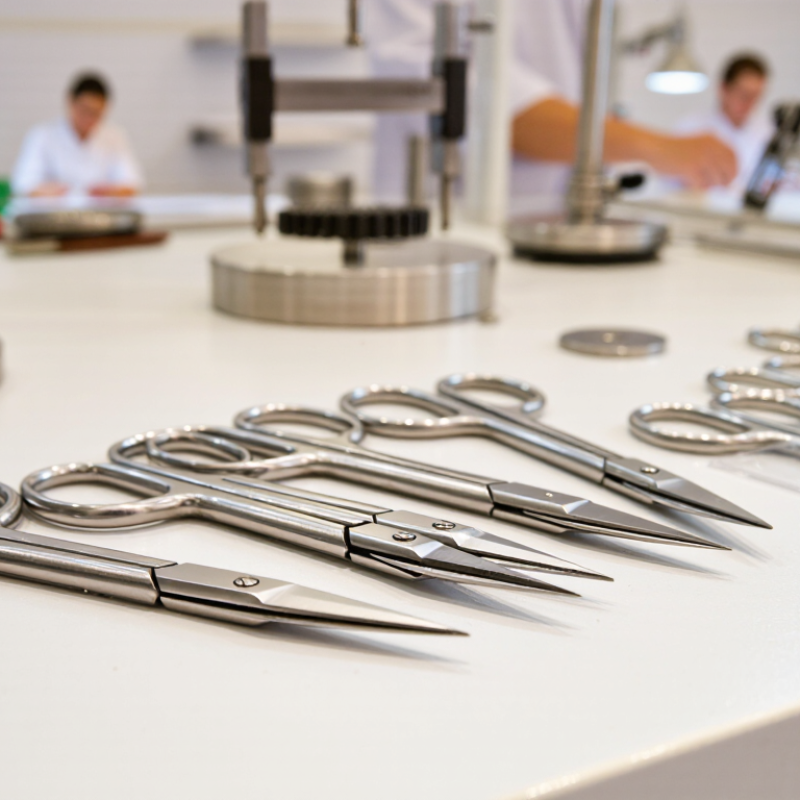
Small details matter. The blades should meet cleanly without visible gaps. Their tips must remain precise, not dangerously pointed or uneven. Stainless steel quality affects corrosion resistance, polishing, and long-term comfort. A well-designed tension screw can support smoother movement during repeated use. Buyers should also examine handle balance, jaw alignment, surface finishing, and protective packaging. Sample testing remains essential. A beautiful sample does not always represent every production batch.
Factory visits, third-party inspections, and documented quality procedures can improve purchasing confidence. Useful evidence may include material records, inspection reports, production photographs, and customer references. However, certificates alone cannot prove excellent cutting performance. They need practical verification. Manufacturers with export experience often understand packaging, labeling, and communication requirements more clearly, but experience should still be checked carefully. Ask direct questions about minimum order quantities, replacement policies, sharpening support, and lead times.
No factory is perfect. Even experienced suppliers may show weaknesses in finishing or consistency. That is worth admitting. The right choice depends on your target market, budget, order volume, and quality expectations. By comparing technical samples and supplier transparency, this article helps readers identify capable Chinese manufacturers and avoid decisions based only on low prices.
Best Cuticle Scissors Manufacturers in China?
What Defines a Cuticle Scissors Manufacturer Under ISO 9001 and GB/T 3280?
A capable manufacturer treats ISO 9001 as a working system, not a wall certificate. The ISO Survey 2023 recorded 1,265,216 ISO 9001 certificates worldwide. This figure shows adoption, but it does not guarantee sharp, safe scissors. A reliable factory should control supplier approval, incoming steel inspection, forging, grinding, assembly, and final release. Each batch needs traceable records, inspection results, and corrective actions.
GB/T 3280 mainly covers cold-rolled stainless steel sheets and strips. It addresses chemical composition, mechanical properties, surface quality, and dimensional tolerances. Therefore, compliance can support material selection, but it does not certify finished cuticle scissors. Buyers should request the steel grade, mill certificate, heat number, hardness data, and corrosion-test method. Blade symmetry also matters. So does smooth opening. Small burrs can damage delicate skin.
Tips: Ask for a sample inspection report. Check blade alignment under magnification. Test ten or more units, not one. Confirm whether the certificate belongs to the actual production site. A supplier may present excellent documents while controlling subcontracted processes poorly. I have seen paperwork look stronger than the product. That deserves reflection. Require production photos, batch coding, calibration records, and an independent pre-shipment inspection when risk is high.
China’s cuticle-scissors supply is concentrated in several manufacturing regions, not one single industrial city. UN Comtrade and ITC Trade Map classify many of these instruments under HS 8214.20. Their trade tables consistently identify China as a major global supplier in this category. However, customs classification can differ when scissors are shipped within manicure sets.
Guangdong is the strongest cluster for metal cutting tools. Yangjiang factories commonly combine stamping, grinding, heat treatment, polishing, and final assembly. This integrated process supports medium and large orders. Zhejiang, especially Yiwu and nearby hardware districts, offers dense supplier networks and flexible purchasing channels. These factories often handle varied handle colors, packaging formats, and smaller trial quantities.
Jiangsu and Shandong also contribute capable machining suppliers, although their visibility is sometimes lower in export directories. China Customs trade data should be checked by province, product description, and shipment period. HS codes alone can hide mixed shipments. That matters.
A useful audit checks blade alignment, hinge smoothness, closing tension, and corrosion resistance. ISO 9001 certification may support process control, but it does not guarantee cutting performance. I would request recent inspection records and production samples. Supplier directories can look convincing. Factory evidence is better. One weakness remains: public trade reports show export movements, not every workshop behind them.
Best Cuticle Scissors Manufacturers in China?
For Chinese manufacturers, steel hardness deserves careful testing. A 48–58 HRC range is not a simple quality ranking. Hardness measures resistance to indentation, not complete cutting performance. ISO 6508-1 defines the Rockwell C method, commonly used for hardened tool steels. A 48–52 HRC blade usually offers better toughness and easier sharpening. It can tolerate small drops and twisting. However, its edge may dull sooner during repeated salon use.
At 53–58 HRC, the blade often keeps a sharper edge longer. This suits precise cuticle trimming and high-volume professional work. Yet excessive hardness can increase chipping risk. Heat treatment, blade geometry, carbide distribution, and surface finishing matter equally. The ASM Handbook links cutting performance with microstructure, not hardness alone. World Stainless reported approximately 58.4 million tonnes of crude stainless production in 2023, showing the material’s broad industrial scale. That figure does not prove every batch performs consistently. This is where supplier verification becomes important.
Tips: Ask manufacturers for batch-level HRC reports, not only catalog claims. Check testing locations near the cutting edge. Test several samples after repeated opening cycles. A 56 HRC sample may cut beautifully, but poor alignment can still damage skin. I have seen hardness targets look impressive while the pivot feels loose. That detail deserves more attention. Request steel grade, heat-treatment records, blade-gap measurements, and a practical cutting sample before placing a large order.
Rockwell C hardness is a material property, not a complete quality rating. In general, higher hardness improves resistance to edge deformation and wear, while excessive hardness can increase brittleness and the risk of chipping if the blade is misaligned, dropped, or poorly heat-treated.
The chart shows the actual hardness range in HRC and an engineering interpretation of typical blade behavior. Final performance also depends on steel composition, heat treatment, blade geometry, sharpening quality, and joint alignment.
For stainless-steel cuticle scissors, ASTM A967 testing helps verify whether passivation removed free iron and improved corrosion resistance. The standard recognizes several methods, including water immersion, high humidity, salt spray, copper sulfate, and potassium ferricyanide–nitric acid testing. Each method exposes weaknesses differently. Copper sulfate testing can reveal free iron on stainless surfaces, while salt spray provides a harsher corrosion challenge. Acceptance criteria depend on the steel grade, treatment, and product specification.
The World Stainless Association reported approximately 58.4 million tonnes of crude stainless-steel production in 2023. This scale makes consistent surface treatment essential, especially for small instruments exposed to moisture, cleaning chemicals, and repeated handling. In practical inspections, a bright surface can still hide contamination around joints, blades, or drilled holes. ASTM A967 testing should therefore use representative samples, not only visually perfect pieces. A passing result is valuable, but it is not a lifetime guarantee. Poor rinsing or abrasive handling can damage the passive layer later.
Tips: Request the exact ASTM A967 test method, exposure time, acceptance criteria, steel grade, and laboratory records. Check whether samples represent finished scissors after polishing and assembly. Consider combining copper sulfate with humidity or salt spray testing. One test may miss a localized problem. Testing is not always elegant, but vague certificates create greater risk. Manufacturers should also review cleaning chemistry, rinse-water quality, and packaging conditions because passivation quality can decline before shipment.
| ASTM A967 Test or Quality Dimension | What It Verifies | Typical Relevance to Stainless-Steel Cuticle Scissors | Acceptance and Reporting Considerations | Recommended Record |
|---|---|---|---|---|
| Water-Immersion Test ASTM A967/A967M |
Checks for visible rust or corrosion products after exposure to heated water, indicating whether the passive surface is sufficiently stable. | Useful for polished blades, finger rings, pivot areas, and other surfaces that may retain moisture during cleaning or storage. | The specification and purchase order should define the exact exposure condition, specimen preparation, inspection time, and allowable corrosion evidence. | Record stainless-steel grade, passivation process, test condition, exposure duration, inspection method, and result. |
| High-Humidity Test ASTM A967/A967M |
Evaluates resistance to corrosion under warm, humid conditions that can reveal inadequate cleaning, iron contamination, or a weak passive film. | Relevant to scissors transported or stored in humid environments, especially where packaging can trap condensation. | Acceptance is normally based on visual examination for rust or corrosion after the specified humidity exposure; criteria must be agreed in advance. | Keep chamber conditions, specimen orientation, exposure time, photographs, and corrosion observations. |
| Salt-Spray Test ASTM A967/A967M |
Challenges the passivated surface with a chloride-containing atmosphere to identify corrosion susceptibility and process inconsistency. | Helpful for products exposed to perspiration, saline moisture, coastal shipping conditions, or repeated handling. | Salt spray is a comparative screening tool and should not be treated as a direct prediction of service life. The test duration and corrosion limit should be specified. | Document salt solution, chamber parameters, exposure duration, inspected areas, corrosion rating, and test photographs. |
| Copper-Sulfate Test ASTM A967/A967M |
Detects free iron or iron contamination on stainless-steel surfaces through the formation of deposited copper. | Particularly useful for blades and pivot components that may have contacted carbon-steel tooling, abrasive media, or contaminated handling equipment. | Copper deposition generally indicates a failure. The method has limitations for some stainless-steel grades and should be selected according to the material and standard requirements. | Record alloy designation, surface condition, reagent details, exposure time, visible copper deposition, and disposition. |
| Potassium-Ferricyanide–Nitric-Acid Test ASTM A967/A967M |
Provides a sensitive indication of free iron or iron contamination on stainless-steel surfaces. | Suitable for investigating contamination on fine-cut edges, recessed pivot holes, and polished surfaces where visual inspection alone may be insufficient. | Because the reagents are hazardous and the test is sensitive to method control, it should be performed by trained personnel using the applicable ASTM procedure and safety controls. | Record reagent preparation, test area, reaction or color change, operator, laboratory conditions, and pass/fail decision. |
| Passivation Process Verification | Confirms that the treatment route, chemical concentration, temperature, time, rinsing, and drying controls are consistent with the specified stainless-steel grade. | Helps prevent staining, flash rust, chemical residue, and premature corrosion on scissors after grinding, polishing, ultrasonic cleaning, or assembly. | ASTM A967/A967M permits multiple passivation treatments; the selected treatment and verification test should be agreed between purchaser and processor. | Retain batch number, material certificate, process parameters, bath analysis, rinse-water control, operator, and release approval. |
| Stainless-Steel Grade and Material Traceability | Confirms that the material chemistry and grade used for the blades, handles, and pivot parts match the purchase specification. | Different stainless-steel grades have different corrosion resistance, hardening behavior, edge retention, and passivation response. | ASTM A967/A967M does not replace material verification. Use a material certificate and, when required, positive material identification or laboratory chemistry testing. | Record heat or lot number, grade, supplier certificate, chemical composition, and component-to-batch traceability. |
| Post-Passivation Cleanliness and Visual Finish | Checks for residual acid, salts, abrasive particles, fingerprints, discoloration, burrs, and surface damage after passivation and rinsing. | Important for sharp cutting edges, polished exterior surfaces, finger rings, and moving joints that must remain clean and smooth. | Define lighting, magnification, viewing distance, allowable marks, edge condition, and cleaning requirements in the inspection plan. | Record inspection standard, sampling plan, defect classification, photographs, rework status, and final release result. |
Choosing a cuticle scissors manufacturer in China requires more than comparing unit prices.
MOQ, lead time, and OEM depth often decide the real cost. A practical MOQ may range from 500 to 3,000 pieces, depending on steel grade, handle design, and packaging. Lower quantities usually increase tooling and inspection costs. A low MOQ is not always a win.
A 15–30-day lead time is realistic for repeat orders with approved specifications. It becomes less reliable for new molds, custom polishing, or complex retail packaging. The World Bank’s 2023 Logistics Performance Index ranked China 19th globally, showing strong logistics capability but not eliminating port delays. UNCTAD’s Review of Maritime Transport reports that ships carry over 80% of global merchandise trade.
Therefore, production time is only part of the schedule. Add inspection, export handling, and ocean transit. My experience suggests buyers should request a dated production plan, not a verbal promise. Suppliers should also explain how they control blade alignment, spring tension, and corrosion resistance.
Tips:
Ask for a pilot order before committing to a large MOQ. Confirm whether samples use production-grade steel. Request inspection photos, carton dimensions, and a written replacement policy. OEM services should include logo engraving, packaging artwork, color matching, and barcode support. However, each addition can extend the timeline. Leave several buffer days. That detail is often overlooked.
It shows a controlled quality system, not guaranteed cutting performance. A factory should track suppliers, steel, forging, grinding, assembly, and final inspection. Records should include batch codes, inspection results, and corrective actions. Certificates alone are not enough.
No. It mainly covers cold-rolled stainless steel sheets and strips. The standard addresses composition, mechanical properties, surface quality, and dimensions. Ask for the steel grade, mill certificate, heat number, and hardness data. The finished scissors still need separate inspection.
Request production photos, batch coding, calibration records, and sample inspection reports. Also request heat-treatment records and blade-gap measurements. Check whether documents belong to the actual production site. Paperwork can look stronger than reality.
Test at least ten units, rather than trusting one attractive sample. Check blade alignment under magnification. Look for burrs, uneven edges, loose pivots, and rough opening. Test repeated opening cycles. One sample can mislead.
Lower hardness often provides better toughness and easier sharpening. Higher hardness may preserve sharpness during repeated professional use. However, excessive hardness can increase chipping risk. Hardness is only one factor.
No. Cutting performance also depends on heat treatment, geometry, microstructure, and alignment. A 56 HRC blade may feel excellent but still damage skin when poorly aligned. Do not judge quality from one number. That deserves reflection.
Symmetrical blades help create a controlled cutting path. Smooth opening reduces snagging and uneven pressure near delicate skin. Small burrs may cause discomfort or minor skin damage. Inspect the pivot closely.
It is useful when order value, production risk, or subcontracting risk is high. An inspector can verify batch quantity, markings, dimensions, and cutting performance. They can also compare actual goods with approved samples. It cannot replace good supplier control.
Choosing the best cuticle scissors manufacturers in China requires evaluating quality systems, materials, production capability, and service terms. A reliable manufacturer should operate under ISO 9001 and follow relevant GB/T 3280 stainless-steel requirements, with documented inspection from raw material selection to final assembly. Major manufacturing regions, including Zhejiang, Jiangsu, and Guangdong, supply products commonly classified under HS 8214.20. Buyers should also confirm whether the manufacturer can provide consistent blade hardness between 48 and 58 HRC, as this range influences sharpness, durability, flexibility, and resistance to deformation.
For stainless-steel cuticle scissors, ASTM A967-based passivation verification may include chemical passivation procedures and tests such as water immersion, high-humidity exposure, or copper sulfate testing, depending on the specification. Commercial terms should be compared carefully: MOQs may vary according to customization, standard production often requires 15–30 days, and OEM services can include logo application, packaging, handle design, and tailored blade finishing. Clear inspection standards, sampling procedures, and delivery commitments help buyers select a dependable supplier.